Leave Your Message

How to Choose Shot Peening Equipment in 2026?

Choosing Shot Peening Equipment in 2026 starts with the part, not the machine brochure. A turbine component with narrow passages needs different coverage than a flat automotive spring. Part size, material, required fatigue performance, and production volume all shape the decision. Small details matter. A fixture that hides a critical surface can undermine an otherwise capable process.

Compare air-blast and wheel-blast systems against your actual workload. Review intensity control, media flow, coverage consistency, dust collection, and media recovery. Ask how operators will load parts and inspect process records. Automation may improve repeatability on high-volume lines, but it can add cost and maintenance needs. A manual cabinet may suit varied, lower-volume work better. It depends.

Request a demonstration using representative parts and media, then check the results against your documented specifications. Confirm that the supplier can explain calibration, routine maintenance, and operator training in practical terms. Do not rely on a headline capacity figure alone; cycle time can change with part geometry and loading. I would also leave room for a second review. Equipment choices are sometimes made before the production mix is fully understood. This guide outlines the questions that help buyers compare systems carefully, identify trade-offs, and choose Shot Peening Equipment that fits both current needs and realistic plans for growth.

How to Choose Shot Peening Equipment in 2026?

Understanding Shot Peening Equipment and Its Main Functions

How to Choose Shot Peening Equipment in 2026?

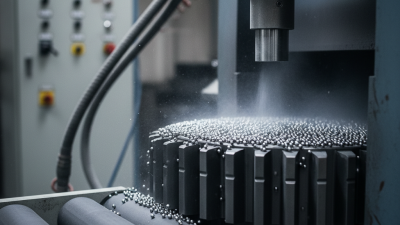
Shot peening equipment improves fatigue resistance by striking metal surfaces with controlled abrasive media. Its main function is not simple cleaning. It creates compressive stress beneath the surface, helping parts resist cracks and repeated loads.

In practical trials, I check the machine’s blast method, media flow, coverage, and intensity control. Air-blast cabinets suit smaller or complex components. Wheel-blast systems often handle higher production volumes. Both systems need stable pressure or wheel speed. They also require accurate abrasive metering. Small changes can affect the final stress profile.

Look closely at the dust collector. Poor extraction can reduce visibility and contaminate the workspace. An effective separator removes broken media and keeps reusable particles consistent. Automatic part rotation can improve coverage on curved surfaces. Manual loading may be cheaper, but it can produce uneven results. I once found missed areas beneath a part fixture. The machine was not the only problem. The setup was.

Choose controls that record pressure, wheel speed, exposure time, and media condition. Almen strip testing can verify peening intensity instead of relying on appearance. Keep calibration records and inspect nozzles, liners, seals, and filters regularly. Operator training matters too. A sophisticated machine still performs poorly when settings are guessed. In 2026, practical equipment should support traceable data, efficient media use, ergonomic access, and straightforward maintenance. A perfect setup is rare. Careful verification remains essential.

Defining Surface Treatment Goals and Process Requirements

How to Choose Shot Peening Equipment in 2026?

Defining Surface Treatment Goals and Process Requirements

Surface treatment starts with the part, not the machine. Define the required fatigue life, surface hardness, roughness, and corrosion resistance before comparing equipment. In production trials, I record material grade, geometry, masking areas, and the starting surface condition. A polished panel and a cast housing will not respond in the same way. State target values clearly, such as coverage percentage, peening intensity, roughness range, and allowable dimensional change. Keep it measurable.

Process details determine the equipment configuration. Consider part size, loading method, cycle time, media diameter, and media recovery needs. Complex cavities may require adjustable nozzles, multiple angles, or controlled part rotation. Thin sections need gentler settings and careful monitoring. Dust extraction also matters, especially in enclosed work areas. It is not a minor accessory. Check whether the machine can maintain stable air pressure, media flow, and nozzle distance during long cycles.

Use trial data to confirm the choice. Measure intensity with certified test strips, inspect coverage under magnification, and verify dimensions afterward. A neat spreadsheet can still hide uneven treatment. I have seen operators trust nominal settings while shadowed edges remained untreated. My own early assessments sometimes focused too much on output speed. That was a mistake. Ask for maintenance records, calibration methods, operator training, and documented process controls. Leave room for adjustment; real parts rarely behave perfectly.

How to Choose Shot Peening Equipment in 2026? – Defining Surface Treatment Goals and Process Requirements

Decision dimension What to define Equipment implications Practical verification
Surface treatment goal Identify whether the priority is fatigue-life improvement, residual compressive stress, surface cleaning, or preparation for a subsequent coating or process. Choose a peening system when controlled impact treatment is required. Do not treat cleaning or coating preparation as interchangeable with a qualified peening process. Set measurable acceptance criteria for the application, such as specified intensity, coverage, surface condition, and process records.
Part geometry and access Record part size, mass, surface curvature, recesses, holes, edges, and the areas that must be treated or masked. A manual or robotic air-blast cabinet can suit localized or complex surfaces. A wheel-blast machine is generally better suited to repeatable processing of compatible parts with accessible surfaces and suitable loading arrangements. Confirm line-of-sight access, fixture clearance, nozzle or wheel reach, and the ability to prevent unintended treatment of restricted areas.
Required intensity and coverage Define the required peening intensity and coverage from the part specification or validated process. Intensity and coverage are different process measures. Select equipment with stable, adjustable media flow, air pressure or wheel operation, exposure time, and part motion. Ensure the system can repeat the qualified process window. Use Almen strips and a saturation curve to establish intensity where required. Verify coverage using the applicable inspection method and procedure.
Media type and condition Specify media material, shape, size range, hardness where applicable, cleanliness, and permitted media breakdown or contamination limits. Provide compatible media storage, metering, screening, separation, and replenishment. Wheel and air-blast systems may require different media delivery and recovery arrangements. Check media size distribution and condition at defined intervals; remove broken or contaminated media according to the process plan.
Production volume and flexibility Estimate parts per shift, batch size, changeover frequency, product mix, and expected future capacity. Manual systems offer operator flexibility for varied work. Programmable or robotic systems support repeatable paths for recurring complex parts. Automated systems can improve throughput for suitable, consistent production. Run representative parts at the required takt or batch rate and include loading, fixturing, inspection, and changeover time in capacity calculations.
Process control and traceability Determine which parameters must be recorded, such as recipe, media flow, pressure or wheel settings, exposure time, part identification, and inspection results. Consider recipe control, parameter monitoring, alarms, interlocks, data logging, and controlled access to process settings when required by the quality system. Review sample records and confirm that key settings can be tied to the processed part or batch.
Facility and operator requirements Assess available floor space, electrical supply, compressed-air capacity where needed, ventilation, noise limits, material handling, and operator access. Include dust collection, enclosure integrity, guarding, safe loading, and ergonomic access in the installation plan. Utility demand depends on machine design and operating conditions. Confirm site requirements with the equipment specification and complete a facility, safety, and environmental review before installation.
Maintenance and lifecycle cost Estimate costs for media, wear parts, filters, energy, labor, calibration, planned downtime, and service access over the expected equipment life. Favor designs with accessible inspection points, clear wear-part replacement procedures, maintainable dust collection, and available technical support. Compare total operating cost and planned maintenance requirements, not purchase price alone.
Qualification and acceptance Identify applicable customer, industry, or internal requirements, including qualification, operator training, inspection, and change-control expectations. Choose a system that can support the documented process and required qualification evidence. Equipment alone does not establish process compliance. Plan trials on representative parts, document the approved process window, and define requalification triggers before production release.

Final equipment selection should be based on the part specification, validated process trials, production needs, and applicable safety and quality requirements.

Comparing Equipment Types, Capacities, and Control Systems

How to Choose Shot Peening Equipment in 2026?

Comparing Equipment Types, Capacities, and Control Systems

Equipment type should follow the workpiece, not the sales brochure. Wheel-blast machines suit steady batches of similar components. Air-blast systems offer better access to narrow surfaces and complex geometries. Table, barrel, and continuous systems each handle different loading patterns. A barrel machine may protect labor costs, but it can mark delicate parts through repeated contact. That detail is easy to overlook.

Capacity means more than chamber size. Check the usable load, media flow, recovery rate, and changeover time. A large cabinet can still perform poorly when parts block one another. Measure actual throughput with representative components. Include loading, unloading, masking, and inspection time. Short trials are useful, but they may hide maintenance delays. That is a weakness.

Control systems determine repeatability. Basic manual controls can work for stable, low-volume production. Modern PLC-based systems provide recipes for pressure, wheel speed, exposure time, and media replenishment. Sensors can monitor airflow, abrasive level, and machine faults. Useful systems also record batch data and alert operators before coverage or intensity drifts. Ask for calibration procedures, test coupons, and accessible service records. A complicated interface is not automatically a reliable one. Operators need clear screens, physical safeguards, and practical training. Fancy automation can still fail when measurement discipline is weak.

Evaluating Media Compatibility, Safety, Maintenance, and Energy Use

How to Choose Shot Peening Equipment in 2026?

Evaluating Media Compatibility, Safety, Maintenance, and Energy Use

Choosing shot peening equipment in 2026 requires more than comparing cabinet size or purchase price. Start with media compatibility. Verify the machine supports your selected shot material, diameter, hardness, and flow rate. Incorrect media can damage surfaces, clog recovery systems, or produce uneven coverage. Request test results using your actual components, not generic samples. Small differences matter.

Safety should be practical, measurable, and visible. Inspect enclosure interlocks, dust extraction, emergency stops, noise levels, and operator access. A clear viewing window helps workers identify abnormal media flow before problems grow. Ask for documented risk assessments and maintenance instructions. Do not accept vague safety claims. Check them.

Maintenance affects production more than many buyers expect. Look for accessible wear parts, simple media separation, and clear inspection points. Daily checks should cover hoses, nozzles, seals, filters, and recovery screens. In shop trials, teams often underestimate dust-filter replacement time. That mistake becomes expensive during busy shifts.

Energy use deserves closer attention. Compare motor power, compressed-air demand, recovery efficiency, and standby consumption under real operating conditions. A smaller machine may use less power but require longer processing cycles. Record actual energy per completed component. I would also question optimistic supplier estimates. They can miss loading delays, cleaning time, and operator habits. Choosing equipment is partly technical judgment, and partly honest observation.

Selecting a Reliable Shot Peening Equipment Supplier in 2026

Choosing shot peening equipment in 2026 starts with the supplier, not the machine brochure. A reliable supplier should explain how equipment controls intensity, coverage, media flow, and part positioning. Ask for process records from similar components. Request a live trial with your actual material, geometry, and target specification. A polished demonstration is not enough. Real parts reveal awkward corners, masking issues, and uneven coverage.

Look for engineers who can discuss Almen strips, saturation curves, nozzle distance, wheel speed, and media classification. Their answers should be practical, not copied from a sales sheet. Confirm calibration procedures, inspection frequency, software access, and data export options. Traceable records matter when production results change months later. Check whether the supplier provides training, maintenance instructions, critical spares, and responsive technical support. A machine can be strong, yet idle without those details.

Supplier evaluation should include factory references, documented quality practices, installation planning, and clear acceptance criteria. Ask who handles service after commissioning and how quickly problems are escalated. I have seen teams focus on purchase price and underestimate media contamination or operator learning time. That mistake becomes expensive. No supplier is perfect. The honest ones admit limitations and suggest tests before promising performance. Leave room for independent verification.